For most modern or replacement PWR steam generators, Alloy 690TT is the leading low-SCC-risk tube route. Alloy 800NG is a proven but OEM- and fleet-specific nuclear-grade modification of N08800, not ordinary Alloy 800. Legacy Alloy 600 must be separated into mill-annealed 600MA and thermally treated 600TT. Final selection still depends on steam-generator design, water chemistry, fabrication, qualification, and the project code of record.
PWR STEAM-GENERATOR TUBE MATERIAL DECISION GUIDE
Treat the tube as an approved material state, manufacturing route, inspection package and project qualification—not as an alloy name alone.
1. What is actually being selected?
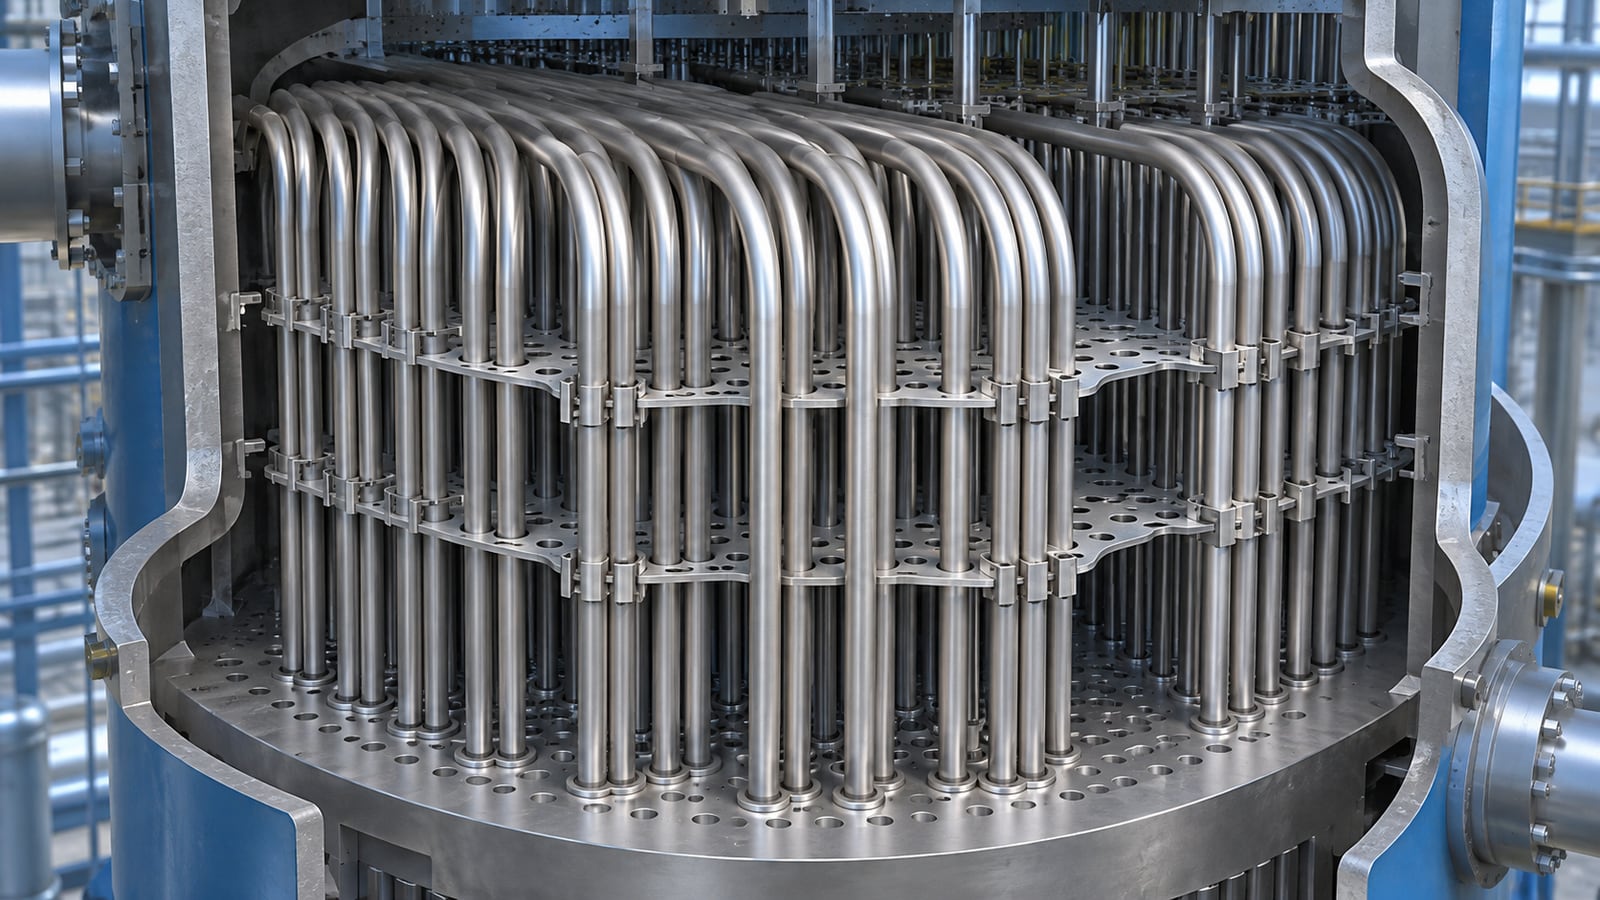
A PWR steam generator tube purchase is not a simple choice among three alloy names. The accepted product is a controlled combination of:
- a base alloy and exact UNS designation;
- a defined material condition, such as 690TT, 600MA, or 600TT;
- an approved melting, tube-making, heat-treatment, finishing, and examination route;
- the applicable construction code and project edition;
- OEM, owner, regulator, and steam-generator manufacturer requirements; and
- a qualified supplier route with the required quality records and approvals.
That distinction matters because a certificate showing UNS N06690 does not, by itself, prove that the tube is qualified Alloy 690TT steam-generator tubing. The same is true for UNS N08800 and Alloy 800NG. The material name identifies the starting chemistry family; it does not prove the final microstructure, residual-work condition, eddy-current response, quality program, or project acceptance.
This article is limited to seamless heat-transfer tubing for pressurized-water-reactor steam generators. It does not transfer directly to CANDU/PHWR, VVER, HTGR, sodium-cooled reactor, helical-coil SMR, conventional boiler, or general process-heat-exchanger service. Those systems can use different designs, environments, inspection rules, and failure histories.
2. Why the material condition is as important as the alloy name
The useful comparison is 690TT versus 800NG versus 600MA versus 600TT, not “690 versus 800 versus 600.” Heat treatment and manufacturing history change grain-boundary carbide distribution, residual stress, cold work, surface condition, and therefore susceptibility to stress-corrosion cracking.
| Tube route | What the designation should mean | Appropriate procurement interpretation | Main limitation |
|---|---|---|---|
| Alloy 690TT | UNS N06690 with a controlled final mill anneal, thermal treatment, microstructure, cold-work limit, surface condition, and nuclear steam-generator acceptance route | The prevalent modern PWR choice where it is supported by the OEM and project licensing basis | Excellent field SCC history does not eliminate wear, vibration, deposits, chemistry excursions, or damage from fabrication |
| Alloy 800NG | An OEM- or project-defined nuclear-grade modification of N08800 with narrowed chemistry and controlled processing | A valid long-service route in specified Siemens/KWU and other approved designs | There is no single universal ASTM definition of “800NG”; generic N08800 is not automatically equivalent |
| Alloy 600MA | Mill-annealed UNS N06600 used extensively in early Western PWRs | A legacy condition essential to ageing and replacement decisions | Extensive primary- and secondary-side degradation history makes it an unsuitable generic benchmark for new procurement |
| Alloy 600TT | Thermally treated UNS N06600 with improved grain-boundary condition compared with 600MA | A distinct legacy route with better SCC performance than 600MA | It is not equivalent to 690TT and still requires condition-specific ageing and inspection management |
NRC operating summaries distinguish Alloy 600 from Alloy 690 and explain why thermally treated 690 became the predominant tube material in the U.S. PWR fleet.[1] IAEA ageing guidance likewise treats alloy condition, manufacturing, water chemistry, and steam-generator design as an interacting system rather than independent variables.[2]
3. Why Alloy 690TT leads many modern PWR programs
Alloy 690 contains substantially more chromium than Alloy 600. In the correctly processed TT condition, that chemistry and grain-boundary condition provide much better resistance to the primary-water and secondary-side stress-corrosion mechanisms that drove degradation in earlier Alloy 600 tube fleets. The operational evidence is strong, but it must be quoted with its date and scope.
NUREG-1841 reviewed U.S. operation through December 31, 2004. It covered 577,070 thermally treated Alloy 690 tubes and approximately 173 cumulative calendar years of operation. Only 333 tubes, about 0.06%, had been plugged; most plugging occurred before service, the leading in-service degradation cause was wear at supports or from loose parts, and the review reported no corrosion or cracking degradation in the period evaluated.[3] These are historical operating results, not a guarantee for a new plant or an unlimited-life claim.
The later EPRI Materials Degradation Matrix, Revision 5, continues to report no field SCC instances for Alloy 690TT steam-generator tubing while retaining potential concerns from adverse chemistry, lead contamination, cold work, and long exposure.[4] Laboratory work has also demonstrated that scratches, localized strain, and severely cold-worked regions can change cracking behavior.[5] The engineering conclusion is therefore precise: 690TT has the strongest documented field SCC performance among the compared routes, but “field SCC not observed in the cited dataset” must never be shortened to “immune to cracking.”
The TT suffix is part of the acceptance basis. The April 1999 final EPRI procurement guide for Alloy 690 steam-generator tubing describes final mill annealing at or above 1070 °C followed by thermal treatment at 716 °C, with a +22/−0 °C tolerance, for at least 10 hours.[6] Revision 1 work began in 1998, but the final report was published in April 1999. This is a dated procurement-guide example, not a universal 2026 rule. The project-controlled OEM specification, code edition, qualification program, and approved alternative process govern the actual order.
For procurement, the buyer should therefore request more than a nominal grade:
- the exact final mill-anneal and thermal-treatment requirements;
- the permitted cold work after final heat treatment;
- grain size and grain-boundary carbide acceptance criteria;
- surface finishing and straightening controls;
- heat-treatment records tied to the tube lot;
- full-length nondestructive examination requirements; and
- the required project approvals and record-retention period.
4. Where Alloy 800NG is a valid route
Alloy 800NG has a substantial operating basis in certain PWR steam-generator designs, especially Siemens/KWU fleets, and in some replacement steam generators. The “NG” concept starts with the N08800 family but adds nuclear steam-generator controls. Published fleet studies describe lower carbon, tighter nickel and chromium ranges, titanium stabilization relationships, controlled final cold work, and sometimes surface peening. The exact requirements vary by OEM, generation, and project.[7]
That makes the procurement boundary simple: a generic ASTM B163 N08800 tube and its material certificate do not prove Alloy 800NG conformity. The buyer must supply or identify the controlled OEM or owner specification. A supplier should then map every chemistry, process, dimensional, examination, and documentation requirement against that document.
Long service experience supports 800NG as a technically credible choice within an approved system. It does not establish universal superiority. Published EPRI and IAEA evidence records generally strong performance while also documenting instances of outside-diameter intergranular attack or stress-corrosion cracking associated with deposits, crevices, adverse secondary-water conditions, local stress, or the details of a particular manufacturing route.[2][7] A defensible selection therefore asks whether the exact 800NG route has been qualified for the intended steam-generator design—not whether “Alloy 800” has a good reputation.
Selection between 690TT and 800NG can also be constrained by an installed fleet’s licensing basis, qualified inspection techniques, repair criteria, OEM design, operating chemistry program, and replacement strategy. A purchasing team should not substitute one material solely because a nominal property table looks better. Changing the tube route can affect design analyses, tube-to-tubesheet fabrication, U-bend processing, examination calibration, quality documentation, and regulatory review.
5. Why 600MA and 600TT must remain separate
Alloy 600MA was used widely in early PWR steam generators. Its operating history established much of the industry’s knowledge about primary-water stress-corrosion cracking, outside-diameter stress-corrosion cracking, intergranular attack, pitting, wastage, and denting. That history also drove improvements in water chemistry, tube inspection, support materials, repair criteria, and replacement-steam-generator design.[1][2]
Thermal treatment changes the material condition. Alloy 600TT has a more favorable grain-boundary carbide distribution and generally better SCC performance than 600MA. NRC NUREG-1771 documents U.S. experience with thermally treated Alloy 600 and the inspection implications for plants with a demonstrated absence of cracking.[8] However, 600TT still has reported primary- and secondary-side SCC experience under certain conditions. It can also suffer fretting, denting, wear, and damage associated with residual stress, inadequate treatment, lead contamination, deposits, or unfavorable design details.[2]
For an operating plant, the exact material condition changes the degradation assessment and inspection program. For a new procurement comparison, legacy 600MA and 600TT are mainly historical and engineering baselines. They should not be merged into one “Alloy 600” performance number, nor should 600TT be presented as equivalent to 690TT simply because both include thermal treatment.
6. Failure modes that the alloy comparison must cover
SCC resistance is central, but it is only one part of tube integrity. A credible material-selection review maps the main damage mechanism to its driving environment, stress source, location, and detection method.
| Degradation mechanism | Causal chain | How alloy choice changes the risk | Required controls and verification |
|---|---|---|---|
| Primary-water SCC (PWSCC) | High-temperature primary water + susceptible microstructure + tensile stress or residual cold work → intergranular initiation and growth | 600MA has the most adverse legacy history; 600TT improves it; 690TT has the best cited field history; 800NG performance must be evaluated by route and design | Heat-treatment and microstructure records, cold-work limits, U-bend/tubesheet process controls, qualified ECT, water-chemistry control, and in-service inspection |
| ODSCC and intergranular attack | Deposit or crevice concentration + acidic/alkaline species, sulfur, chloride, lead, or redox imbalance + stress → OD intergranular attack/cracking | 690TT reduces susceptibility relative to legacy 600 conditions but is not a license to ignore deposits; 800NG performance remains system-specific | Secondary-water chemistry, impurity limits, deposit monitoring/removal, focused tube-support and tubesheet inspection, and mechanism-specific probes.[14] |
| Denting | Corrosion-product growth around carbon- or low-alloy-steel supports/tubesheet + constrained geometry → tube deformation and high local stress | Tube alloy alone cannot remove the cause; support material, chemistry, crevice geometry, and deposits dominate | Support design/material, chemistry control, dimensional monitoring, ECT trending, and repair decisions based on the plant program |
| Fretting and support wear | Flow-induced vibration + support clearance or intermittent contact → repeated rubbing → wall loss | All four tube conditions can be damaged. NUREG-1841 identified wear as the main in-service issue in its early 690TT population | Thermal-hydraulic and vibration analysis, support/AVB fit-up, manufacturing tolerances, loose-part exclusion, baseline ECT, and periodic sizing |
| High-cycle fatigue | Alternating flow load or unstable dryout-region loading + inadequate support/damping → cyclic stress → cracking or wear-fatigue interaction | A higher-SCC-resistance alloy does not correct a vibration design problem | Design analysis, fatigue evaluation, support verification, and examination of high-response locations |
| Loose-part wear | Foreign object + fluid motion + repeated impact/contact → localized wall loss | Largely independent of SCC ranking | Cleanliness, foreign-material exclusion, secondary-side inspections, loose-parts monitoring, and localized NDE |
| Pitting, wastage, or impingement | Concentrated impurities, historical phosphate chemistry, particles, or local two-phase flow → localized metal loss | Alloy and condition affect resistance, but chemistry and flow remain decisive | Chemistry history, deposit analysis, ECT/UT sizing, cleaning, and flow/foreign-object correction |
Two lessons follow. First, 690TT’s SCC advantage cannot compensate for poor anti-vibration-bar contact, an unfavorable tube-support gap, a retained loose object, or uncontrolled deposits. Second, tube material cannot be ranked independently of the steam-generator system. The IAEA framework connects design, material concept, fabrication, operating chemistry, inspection, and maintenance because each changes the stress–environment–susceptibility combination that produces damage.[2]
7. The material–design–chemistry causal chain
A useful selection model follows the complete causal chain:
Base chemistry and inclusion control → tube conversion and annealing → grain-boundary condition and residual cold work → U-bend/tubesheet fabrication stress → support contact and vibration response → primary- and secondary-side chemistry → deposit or crevice concentration → initiation and growth mechanism → NDE detectability → repair or plugging decision.
Changing one link does not validate the others. For example:
- Selecting 690TT can reduce SCC susceptibility, but an aggressive scratch or severe local cold work can create a less favorable region.
- Selecting 800NG can fit an approved KWU-derived design, but an ordinary N08800 heat certificate does not establish the narrowed chemistry or processing history.
- Improving secondary-water chemistry can reduce impurity concentration, but it cannot remove an existing foreign object or correct inadequate support contact.
- Requiring 100% eddy-current testing can screen for defined indications at manufacture, but it cannot predict all future wear or prove indefinite freedom from SCC.
The correct decision is therefore not “Which alloy has the highest chromium?” It is “Which fully specified and qualified tube route fits this licensed design, its chemistry program, its fabrication sequence, its inspection technology, and its supply-chain evidence?”
8. Manufacturing and acceptance evidence chain
The procurement package should connect each tube to a controlled sequence from melt to final release. A typical evidence chain for evaluation includes:
- Melt and chemistry control. Identify the heat, melting/remelting route, exact UNS, and every project-narrowed element limit. For 800NG, include the controlled definition rather than relying on the suffix alone.
- Hollow production and tube reduction. Record extrusion, cold pilgering or cold drawing, intermediate anneals, reductions, cleaning, and lot segmentation as required by the qualified process.
- Final mill anneal. Record actual metal temperature, duration, atmosphere, line speed or furnace batch, and traceability to the affected tubes.
- Thermal treatment or nuclear-grade route. For 690TT, document the specified TT cycle and any approved deviations. For 800NG, document the exact OEM-defined chemistry, stabilization, final cold work, peening, and heat-treatment requirements.
- Straightening and finishing. Control post-heat-treatment deformation, surface grinding or polishing, cleanliness, dimensional tolerance, and new residual stress.
- Microstructure and mechanical verification. Apply the project sampling plan for grain size, grain-boundary carbides, hardness, tensile properties, and other required tests.
- U-bend manufacturing. Control bend radius, ovality, thinning, surface damage, bend sequence, and any required stress-relief treatment. U-bend acceptance must follow the project design and procedure qualification.
- Nondestructive examination. Perform the specified full-length eddy-current examination and any supplementary methods with approved calibration references, frequencies, signal-to-noise requirements, personnel qualification, procedures, acceptance criteria, and retained data. NRC Generic Letter 97-05 illustrates why detection, characterization, and sizing capability must be tied to a qualified inspection program rather than a generic statement that ECT was performed.[13]
- Serialization and traceability. Maintain the link from heat and process lot to straight tube, U-bend position, heat-treatment record, examination file, marking, packaging, and final data book.
- Witness and release. Observe the agreed hold points, purchaser or authorized-inspector reviews, nonconformance disposition, and final release under the applicable quality program.
Each item needs an objective acceptance criterion. A purchase order that merely says “Alloy 690TT, ASTM B163, nuclear quality” leaves critical variables undefined.
9. What common documents prove—and what they do not
| Document or inspection | It can support | It does not prove by itself |
|---|---|---|
| Material test certificate | Reported heat chemistry, mechanical results, and listed specification tests | A complete 690TT/800NG manufacturing route, nuclear-component code compliance, OEM approval, or service suitability |
| EN 10204 3.1 or 3.2 inspection document | The applicable inspection-document type and stated independent confirmation route | “Nuclear grade,” NQA-1, 10 CFR 50 Appendix B, ASME Section III authorization, RCC-M conformity, or owner approval |
| Positive material identification | Elemental identity within the method’s capability | Carbon at every required level, grain-boundary condition, heat-treatment history, residual stress, or defect freedom |
| Furnace chart and batch record | The recorded time/temperature history for the identified load | Acceptable microstructure at every location or absence of cold work after treatment |
| Metallography report | Sampled grain size or carbide criteria at defined locations | Full-length tube quality or lifetime performance |
| Eddy-current report | Indications detectable under the stated calibration, procedure, equipment, and threshold | Future freedom from SCC, wear, or fatigue; compliance with a different plant’s inspection qualification |
| Third-party witness report | The activities actually witnessed and the referenced acceptance basis | Regulatory licensing, component design approval, or automatic qualification for another project |
These distinctions prevent a common procurement failure: treating a material identity check as proof of a nuclear supply route. Nuclear acceptance requires the specified code, quality program, qualified procedures, authorized parties, traceability, and project approvals together.
10. How ASTM, ASME, regulation, RCC-M, and OEM specifications divide responsibility
ASTM B163-26a covers seamless nickel and nickel-alloy condenser and heat-exchanger tubes, including N06600, N06690, and N08800, within its stated scope.[9] It provides a base product-specification framework. It does not define every 690TT or 800NG nuclear steam-generator requirement.
ASME Section II adopts material specifications such as SB-163 for BPVC use. Section III governs the construction of applicable nuclear facility components under the project’s code of record, component class, edition/addenda, quality requirements, and regulatory conditions.[12] A material listed in Section II is not automatically a completed Section III component, and a supplier should not claim Section III compliance without the precise scope and authorization.
ASME Section XI and plant technical specifications govern in-service examination, flaw evaluation, repair, and replacement within the applicable plant framework. They do not replace the full new-tube procurement specification. In the United States, 10 CFR 50.55a incorporates specified ASME Code editions and NRC conditions. Where §50.55a(b)(1)(xiii) applies, it requires full-length preservice examination of 100% of the tubing in each newly installed steam generator before plant startup and evaluation of revealed flaws against the design specifications.[10]
RCC-M provides rules for the design and construction of mechanical components in PWR nuclear islands.[11] Its application requires the project-designated edition and controlled requirements; a general marketing reference to RCC-M cannot establish compliance. OEM, utility, and steam-generator procurement specifications then add the exact chemistry restrictions, process windows, microstructure, surface, NDE, U-bend, documentation, witness, and approval requirements needed for a specific design.
The invalid shortcut is ASTM B163 certificate = ASME Section III nuclear tube = RCC-M conformity = OEM approval.
Those are different layers. The RFQ and compliance matrix should show which party owns each requirement and which record closes it.
11. A practical selection workflow
Step 1: Fix the design and licensing envelope
Identify the reactor and steam-generator type, new-build or replacement scope, country, regulator, owner, NSSS/OEM, component classification, code of record, and all project specifications. Stop if the design basis is still provisional.
Step 2: Define the degradation environment
List primary-side temperature and chemistry, secondary-water program, expected impurities, deposit and crevice locations, support materials, tube-support geometry, vibration conditions, historical foreign-object risk, and intended inspection access. Separate corrosion drivers from mechanical drivers.
Step 3: Shortlist qualified material states
Compare 690TT, the exact 800NG specification where applicable, and any legacy condition required by the existing design. Do not shortlist generic “690,” “800,” or “600.” Confirm the route is permitted by the OEM, code, and licensing basis.
Step 4: Build the mechanism matrix
For each location—tube expansion, tubesheet crevice, tube-support plate, anti-vibration bar, U-bend, free span, and sludge pile—map PWSCC, ODSCC/IGA, denting, wear, fatigue, pitting, and loose-part damage. Record prevention, detectability, and acceptance strategy.
Step 5: Audit manufacturing feasibility
Review chemistry capability, tube reduction route, annealing/TT capacity, temperature uniformity and recording, post-treatment cold work, surface finish, U-bend capability, metallography, NDE system, calibration, serialization, cleanliness, and packaging. Any proposed deviation needs formal evaluation and buyer approval.
Step 6: Audit the quality and approval route
Confirm the applicable nuclear quality program, authorized inspection, commercial-grade dedication if relevant, supplier qualification, approved vendor status, personnel and procedure qualification, witness points, nonconformance control, document retention, and regulator/OEM/owner approvals. A technically capable tube plant is not automatically an approved nuclear supplier.
Step 7: Freeze the contract acceptance matrix
Turn every material, process, examination, documentation, and approval requirement into a traceable clause with a responsible party and an objective record. Use the hierarchy defined by the contract to resolve differences between ASTM, ASME, RCC-M, OEM, and purchaser documents.
12. Where DAXUN can support the inquiry
DAXUN manufactures nickel-alloy tube products and performs the agreed tube processing within its own production system. For a PWR steam-generator inquiry, DAXUN can first review the submitted material specification, condition, dimensions, process route, inspection plan, traceability, documentation, and delivery requirements for technical and manufacturing feasibility.
This is not a claim that any general tube offer is nuclear-qualified. DAXUN does not represent an item as ASME Section III, RCC-M, NQA-1, NRC, OEM, owner, or utility approved unless the exact authorization, quality scope, supplier status, and project documents establish that fact. If the buyer cannot provide the controlled project or OEM specification, the response must remain a preliminary feasibility review rather than a promise of final nuclear acceptance.
For related baseline alloy information, see DAXUN’s Inconel 600 tube and pipe page and Inconel 625 tube and pipe page. Inspection planning should be agreed in writing; DAXUN’s testing overview explains available verification categories, while the project’s qualified nuclear procedures and acceptance criteria remain controlling.
Send the controlled OEM and project specifications, exact tube condition, dimensions, manufacturing and NDE requirements, nuclear quality clauses, approval route, record package, quantity and destination for a preliminary technical and manufacturing-feasibility review.
13. RFQ information needed before a technical review
Submit the following with the inquiry:
- reactor and steam-generator type, new-build or replacement status, NSSS/OEM, owner, final user, and destination;
- applicable regulator, code of record, component class, ASME/RCC-M edition, project specification, and document precedence;
- exact alloy and condition: 690TT, controlled 800NG specification, 600MA, or 600TT;
- tube outside diameter, nominal and minimum-wall basis, straight length, U-bend geometry, bend radius, quantity, and serialization plan;
- melting/remelting, narrowed chemistry, grain-size/carbide, final anneal, TT, U-bend heat treatment, final cold work, peening, and surface requirements;
- mechanical, metallographic, corrosion, dimensional, surface, ECT, UT, calibration, signal-to-noise, personnel, and data-format requirements;
- quality-program clauses, source surveillance, hold/witness points, authorized inspection, commercial-grade dedication, owner/OEM approval, nonconformance control, and record retention;
- cleanliness, end protection, packaging, export, schedule, and final data-book requirements.
Send the controlled documents through the DAXUN RFQ contact page. The first response should identify missing inputs and feasibility risks before price and delivery are treated as firm.
Frequently asked questions
Is Alloy 690TT immune to stress-corrosion cracking?
No. NUREG-1841 reports its U.S. operating review through December 31, 2004, and EPRI Materials Degradation Matrix Revision 5 was published in 2024; both support excellent field SCC performance in the populations they evaluate, but they do not prove physical immunity. Severe cold work, scratches, residual stress, abnormal chemistry, deposits, lead, and long exposure remain relevant. Wear and vibration can damage 690TT even when SCC is absent.[3][4][5]
Is Alloy 800NG the same as ASTM B163 N08800?
No. ASTM B163 provides a base seamless heat-exchanger-tube specification. Alloy 800NG is an OEM- or project-defined nuclear-grade route with narrowed chemistry and controlled manufacturing condition. The buyer must identify the exact controlled specification; a generic N08800 MTC is insufficient.[7][9]
Why must Alloy 600MA and 600TT be listed separately?
Thermal treatment changes grain-boundary carbide distribution and SCC behavior. 600TT generally performed better than 600MA, but it has its own ageing history and is not equivalent to 690TT. Combining them hides a material-condition variable that affects inspection and integrity decisions.[2][8]
Does ASTM B163 compliance make a tube nuclear-qualified?
No. ASTM B163 establishes base product requirements. Nuclear project acceptance can additionally require ASME Section III or RCC-M provisions, regulatory conditions, an approved quality program, OEM/owner specifications, qualified NDE, traceability, supplier approval, witness points, and a complete data package.[9][10][11]
Can an EN 10204 3.2 certificate or third-party inspection prove nuclear approval?
No. It can document the specified inspection result and independent confirmation route. It does not automatically establish NQA-1, ASME Section III authorization, RCC-M conformity, regulator approval, or OEM/utility approved-vendor status.
Does choosing 690TT eliminate steam-generator tube wear?
No. Support fit, anti-vibration-bar contact, flow-induced vibration, loose parts, thermal-hydraulic conditions, and fabrication tolerance can produce wear in any of the compared alloys. The early U.S. 690TT operating review found wear to be the leading in-service degradation cause in its dataset.[3]
What is the most important document in an RFQ?
The controlled project procurement specification and its document-precedence list are essential. They connect the exact alloy condition to the code of record, OEM design, manufacturing route, examination, quality program, approvals, and acceptance records. Without them, a supplier can assess only preliminary material and manufacturing feasibility.
Technical Sources
- U.S. Nuclear Regulatory Commission, Backgrounder on Steam Generator Tube Issues
- IAEA-TECDOC-1668, Assessment and Management of Ageing of Major Nuclear Power Plant Components Important to Safety: Steam Generators, 2011 Update
- U.S. NRC, NUREG-1841, U.S. Operating Experience with Thermally Treated Alloy 690 Steam Generator Tubes
- EPRI, Materials Degradation Matrix, Revision 5, 3002030559 (2024)
- Wu et al., Insights into stress corrosion cracking in scratched area of Alloy 690TT steam generator tubes, Acta Materialia 255 (2023)
- EPRI, Guidelines for Procurement of Alloy 690 Steam Generator Tubing, TR-016743-V2R1, Final Report, April 1999
- EPRI, Alloy 800 Steam Generator Tubing Experience, 1024992 (2012)
- U.S. NRC, NUREG-1771, U.S. Operating Experience With Thermally Treated Alloy 600 Steam Generator Tubes
- ASTM International, ASTM B163-26a, Seamless Nickel and Nickel Alloy Condenser and Heat-Exchanger Tubes
- U.S. eCFR, 10 CFR 50.55a—Codes and standards
- AFCEN, RCC-M Design and Construction Rules for Mechanical Components of PWR Nuclear Islands
- ASME, Boiler and Pressure Vessel Code
- U.S. NRC, Generic Letter 97-05, Steam Generator Tube Inspection
- EPRI, PWR Steam Generator Deposit Characterization Sourcebook, 3002002794
Technical Accuracy Statement
This article distinguishes public operating evidence, general material specifications, construction-code responsibilities, and project-specific acceptance. It does not approve a material for a particular nuclear plant, replace the controlled code or OEM specification, establish a supplier’s nuclear qualification, or guarantee service life. The owner, NSSS/OEM, steam-generator designer, authorized parties, and regulator must approve the final material, manufacturing route, inspection plan, and quality evidence.
Last reviewed: September 20, 2026